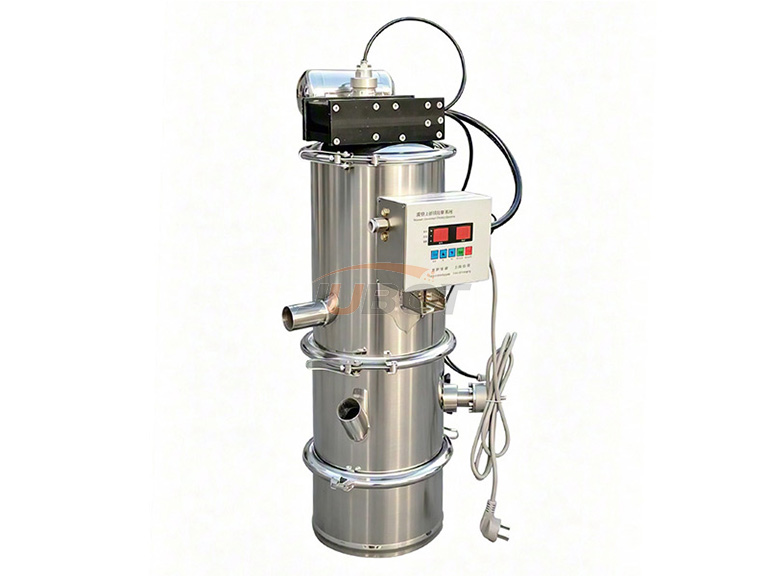
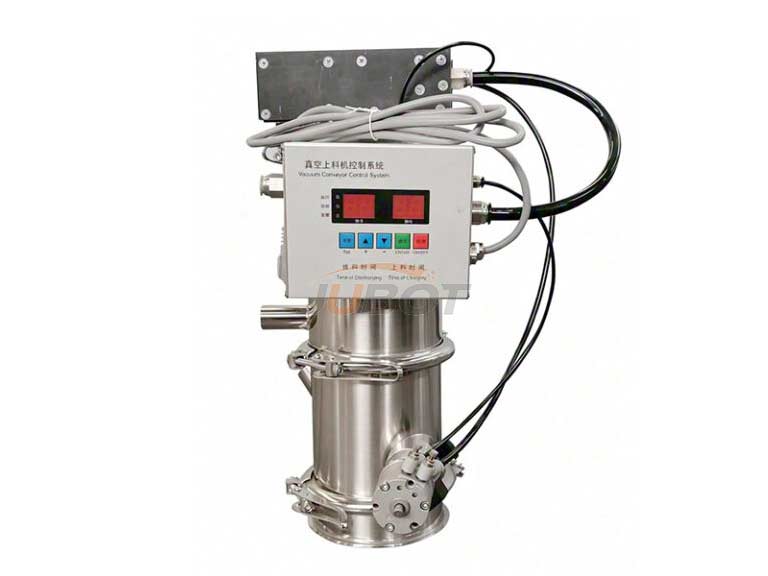
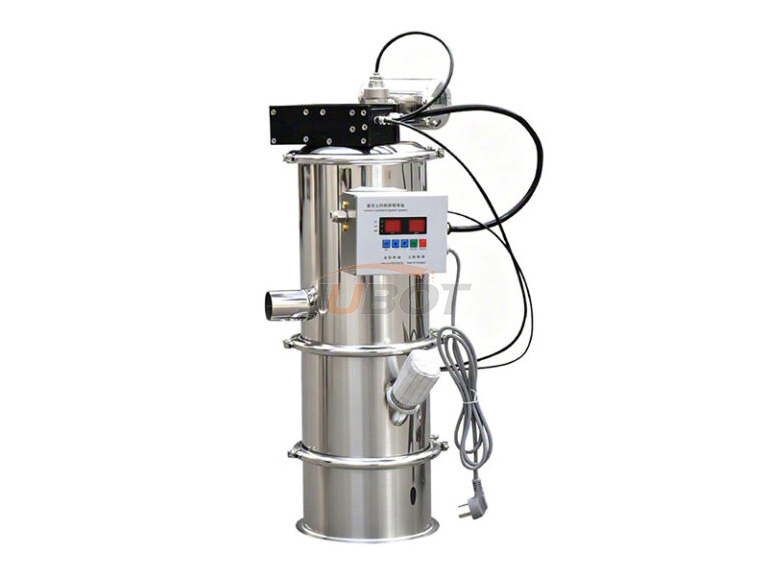
Product Overview
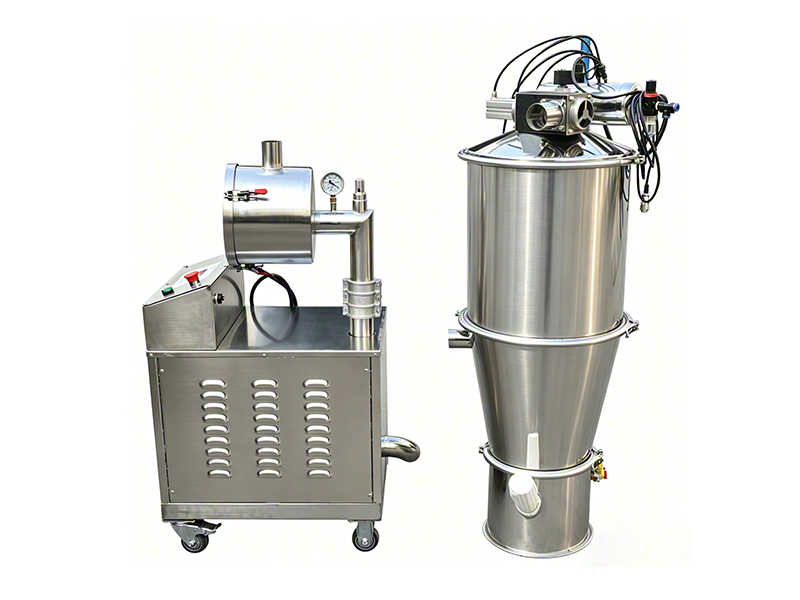
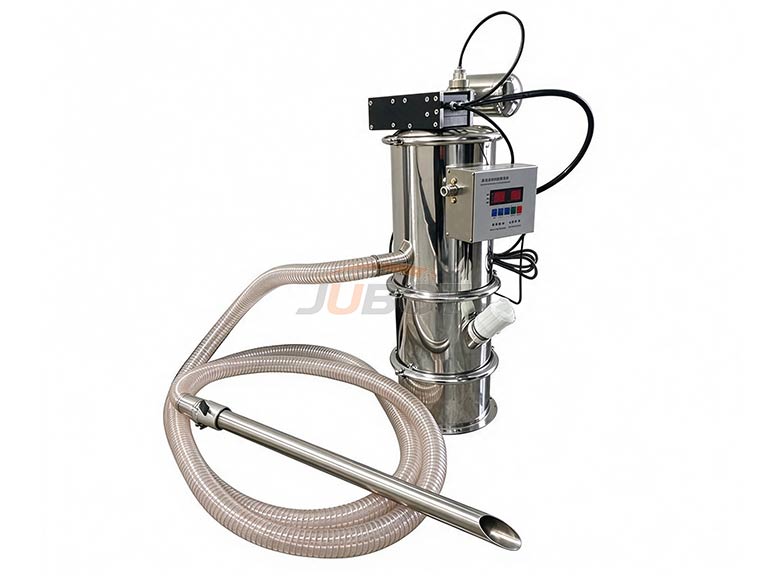
The pneumatic vacuum conveyor is a compressed-air-driven, enclosed conveying device for powders and granular materials. It requires no electrical power and relies on negative-pressure pneumatic conveying to automate material loading. It is widely used in various fine chemical production lines and serves as a core piece of equipment for replacing manual feeding and achieving dust-free production.
Working Principle
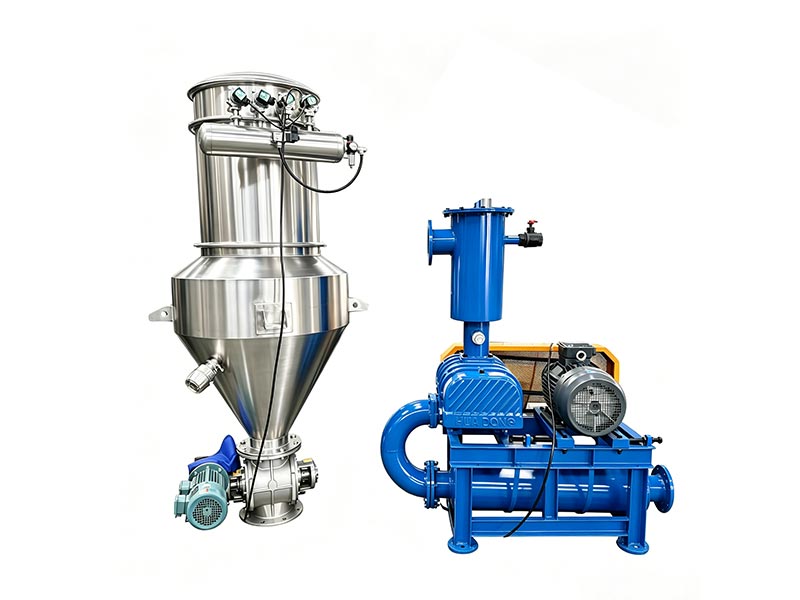
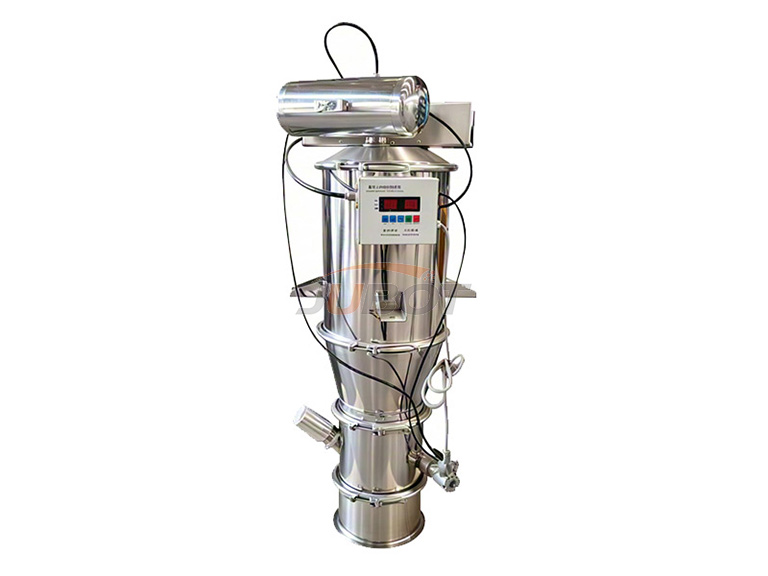
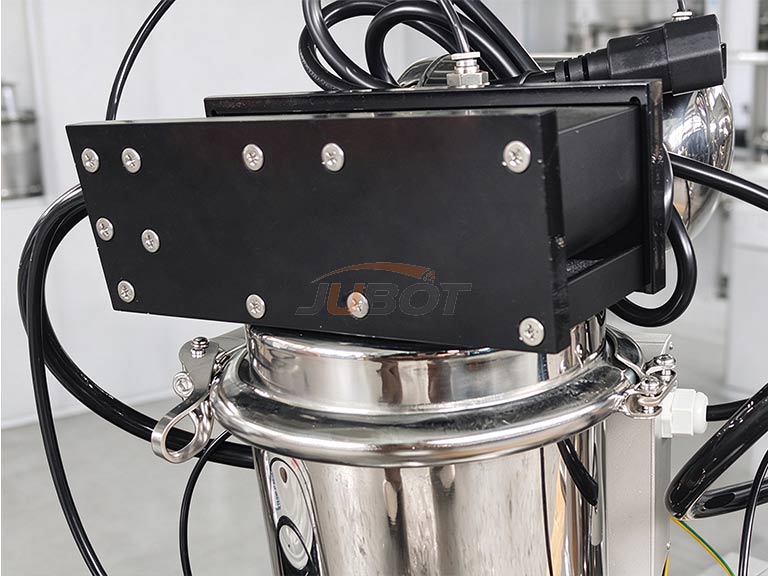
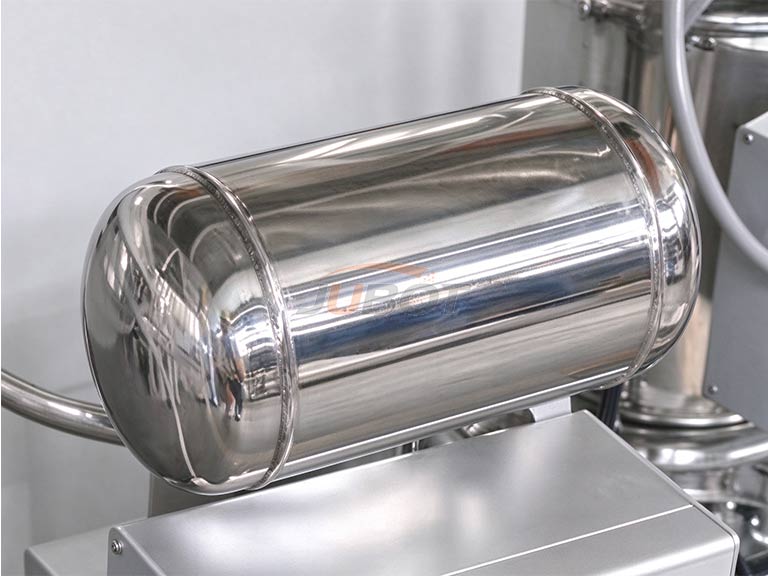
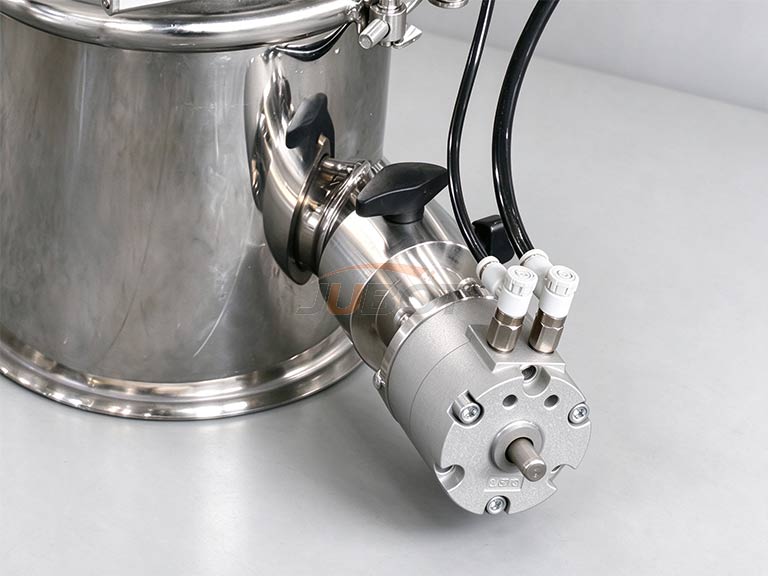
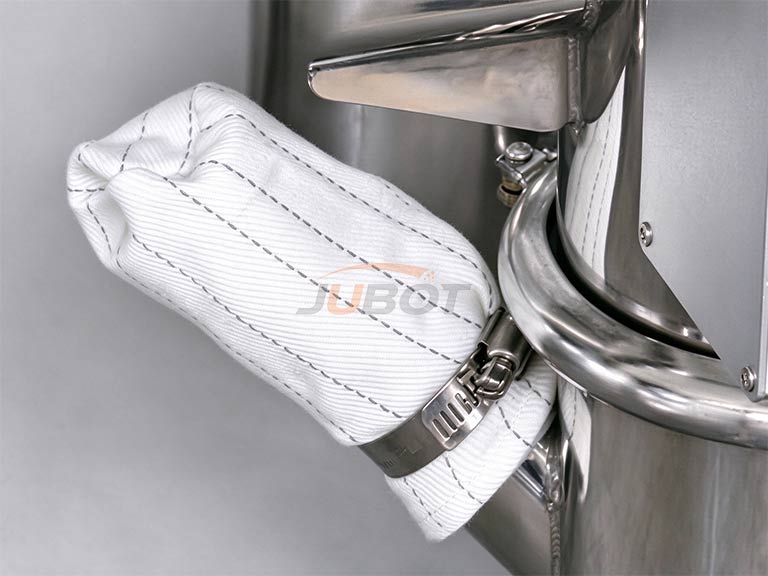
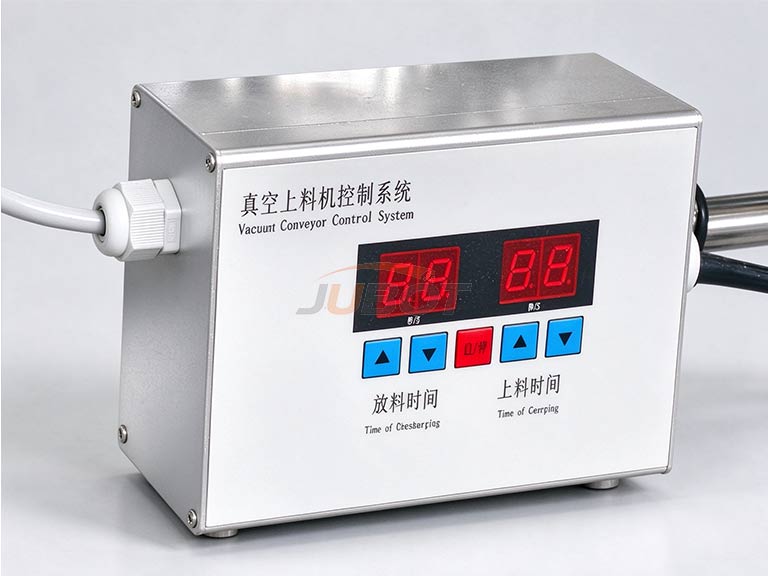
The QVC vacuum conveyor uses a vacuum generator mounted on top to create vacuum, placing the suction nozzle inlet and the entire system under a certain negative pressure. Powder or granular material is drawn into the suction nozzle together with ambient air, forming an air material mixture that travels through the suction hose to the receiving hopper, where air and material are separated. The separated material then enters the downstream receiving equipment. The feeding and discharging cycles are controlled by the opening and closing of a rotary actuator, which is in turn controlled by the electrical control box.
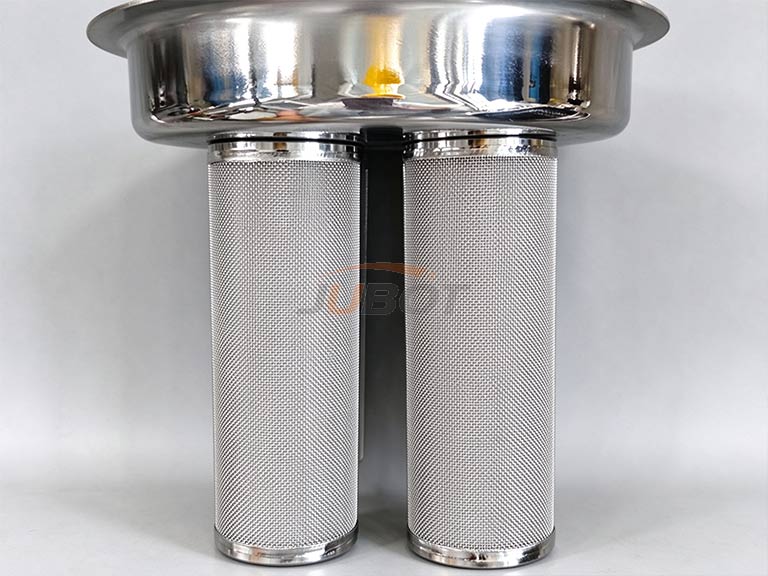
The vacuum conveyor is equipped with a compressed air reverse pulse cleaning system. During each discharge cycle, a pulse of compressed air blows back through the filter element, dislodging accumulated powder from the filter surface to ensure consistent suction performance.
Features and Advantages
The equipment uses negative-pressure pipeline conveying in a completely closed system. Material travels entirely within sealed pipes, eliminating dust leakage and material spillage. This significantly improves the workshop environment and complies with GMP clean-production standards, meeting high cleanliness requirements.
The entire unit is driven by compressed air – no motors, no electrical components, no sparks, and no heat-generating parts, fundamentally eliminating explosion hazards. No additional explosion-proof modifications are required, making it naturally suitable for production processes involving flammable or explosive powders and granules.
With no rotating friction parts and minimal wearing components, the equipment operates with low vibration and low noise, and offers high stability. It can run continuously for extended periods, significantly reducing downtime and maintenance frequency, making it ideal for 24h production.
The system is oil-free and non-contaminating, with no material residue left inside. It is easy to disassemble and clean, effectively preventing cross-contamination between different materials. It meets the high hygiene and purity standards required in pharmaceutical, food, and new energy lithium battery material applications.
The equipment features a high degree of automation – one-touch start/stop, automatic loading, and automatic reverse-pulse filter cleaning to prevent clogging. Routine maintenance is simple, with few consumable parts, greatly reducing labor and maintenance costs.
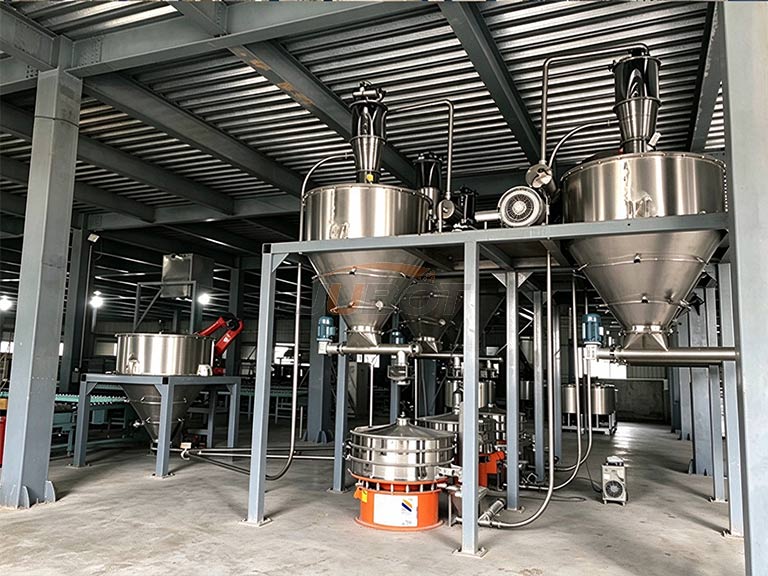
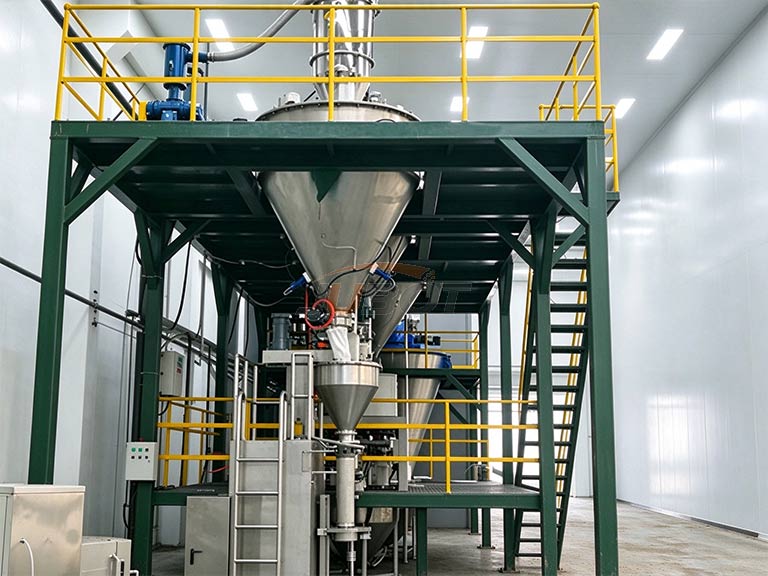
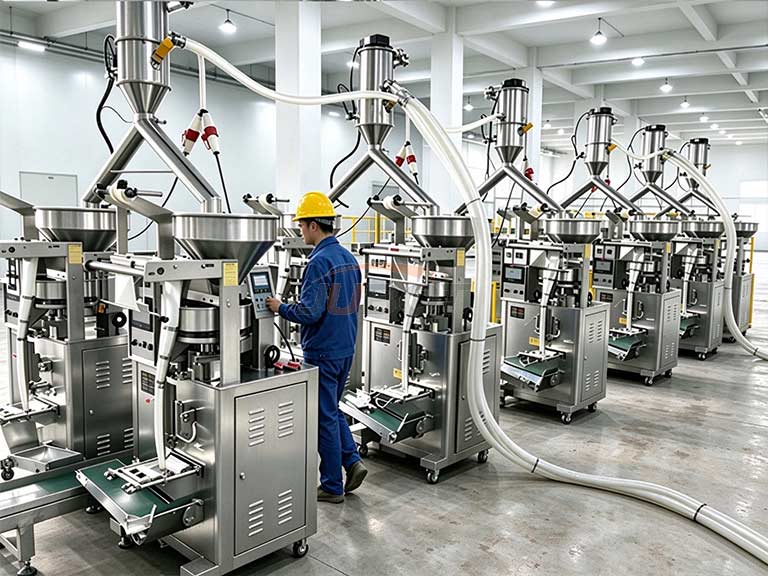
Suitable for various dry powders and fine granular materials, the conveyor can be integrated with mixers, vibrating screens, packaging machines, reactors, and other equipment to achieve fully unattended automated material loading, significantly reducing manual feeding labor.
Applications
Conveying flour, starch, sugar, spices, milk powder, and other food ingredients.
Handling active pharmaceutical ingredients (APIs), excipients, and herbal powders, meeting hygienic and clean requirements.
Transferring pigments, dyes, plastic pellets, catalysts, and other chemical materials.
Conveying cathode and anode materials such as lithium cobalt oxide, graphite, and carbon black.
Conveying cement, quartz sand, calcium carbonate, and other mineral powders.
- Transferring metal powders, ore fines, and other bulk materials.
Specification
| Type | Model | Power Supply (Depending on Region) | Conveying Capacity (Based on Flour) | Hopper Volume (L) | Working Pressure | Tank Diameter × Overall Height |
| Pneumatic | QVC-1 | 380V/50Hz | 50KG | 1.1 | 0.6-0.8MPa | φ140*490 |
| QVC-2 | 380V/50Hz | 100KG | 2 | 0.6-0.8MPa | φ213*790 | |
| QVC-3 | 380V/50Hz | 300KG | 2.4 | 0.6-0.8MPa | φ290*1072 |